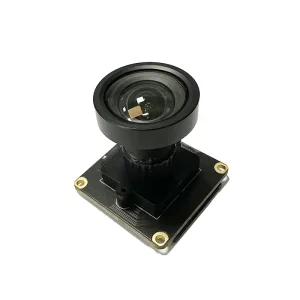
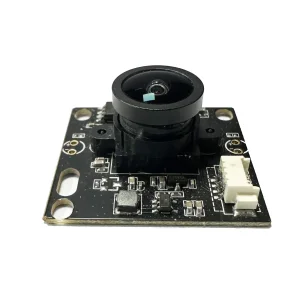
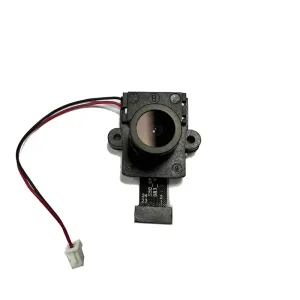
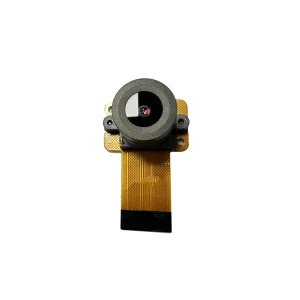
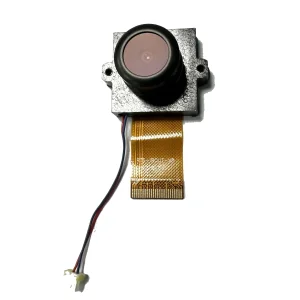
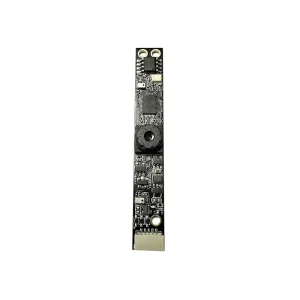
Engineered for seamless system integration, ultra-low distortion, and real-time processing across diverse operational environments.
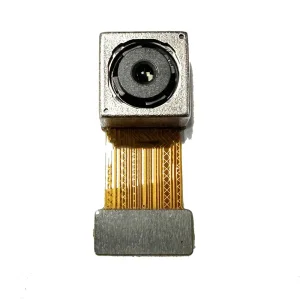
Transitioning from off-the-shelf surveillance units to custom-engineered embedded optical solutions tailored for high-risk, high-precision industrial and commercial applications.
Modern physical security and operational vision infrastructure have moved far beyond standardized consumer-grade security cameras. In today’s complex enterprise ecosystem, top-rated custom security camera systems serve as critical sensory endpoints for AI-driven analytics, perimeter defense, autonomous robot navigation, and industrial process automation. Choosing the right engineering partner and module supplier dictates system reliability, optical fidelity, and long-term total cost of ownership (TCO).
Custom security camera system engineering focuses on eliminating architectural bottlenecks through bespoke optical lens matching, tailored Image Signal Processor (ISP) firmware tuning, customized Flexible Printed Circuit (FPC) layouts, and robust thermal management. As enterprises deploy edge AI microprocessors directly behind the image sensor, the demand for custom MIPI CSI-2, USB 2.0/3.0 UVC, and network-enabled camera modules has experienced exponential growth globally.
Direct tuning of black level calibration, dynamic range compression, automatic white balance (AWB), and noise reduction algorithms specifically adjusted for dynamic real-world lighting environments.
Precision multi-element glass lenses engineered to eliminate optical barrel distortion, ensuring ultra-accurate geometric capture for OCR, document scanning, and facial recognition algorithms.
Module-level potting, wide-temperature (-40°C to +85°C) components, ESD protection circuits, and vibration-proof FPC connections built for continuous industrial operational cycles.
Understanding shifting enterprise demands, compliance mandates, and optical performance benchmarks across key international regions.
The global security camera systems market is undergoing a fundamental transformation driven by three converging macro forces: the proliferation of Edge-AI vision processors, heightened regulatory security mandates (such as NDAA compliance and GDPR edge privacy controls), and the demand for automated visual inspection in smart manufacturing.
Top-rated security camera vendors and system integrators are moving away from monolithic camera assemblies toward modular, component-level custom integration. By embedding custom optics directly into access control turnstiles, smart city kiosks, automatic number plate recognition (ANPR) gantries, and fleet telematics units, OEMs can deliver streamlined industrial design alongside superior imaging performance.
High-Dynamic-Range (HDR) imaging combined with dual-spectrum IR/RGB imaging eliminates backlighting blindness at building entry points, ensuring high accuracy for biometric access and visual doorbells day or night.
Compact, wide-angle, and high-frame-rate driving recorder modules designed to withstand extreme thermal fluctuations inside cabin and chassis environments while capturing flawless video evidence.
Autofocus mini camera modules designed for close-up document scanning, biometric payment authorization, and customer demography analytics operating with standard driverless USB UVC protocols.
A technical examination of image sensor innovations, interface buses, optical coatings, and edge AI integration trends reshaping security systems.
As industrial surveillance requirements become more demanding, the underlying physical hardware must evolve to meet new computational and optical baselines. Key technology roadmaps currently shaping custom camera system manufacturing include:
Adoption of modern BSI (Back-Side Illuminated) and stacked pixel architectures drastically improves quantum efficiency (QE) in near-infrared (NIR) wavelengths (850nm / 940nm), enabling covert, crystal-clear night vision monitoring without dark noise degradation.
Moving beyond legacy DVP parallel buses, modern embedded platforms rely on multi-lane MIPI CSI-2/3 interfaces that directly stream uncompressed RAW pixel data into host NPU/SoC accelerators with sub-millisecond latency.
Replacing traditional threaded manual lens adjustment with 6-axis robotic Active Alignment (AA). By focusing lenses while sensor chip is energized, edge-to-edge optical sharpness is guaranteed across the entire image plane.
Custom camera modules optimized for specific operational constraints, mechanical dimensions, and environmental profiles.
Challenge: High-speed motion blur and severe headlight optical blooming during night monitoring.
Solution: Global shutter sensor modules featuring synchronized strobe LED triggers and high-speed shutter controls (up to 1/10,000 sec) for zero-blur license plate acquisition.
Challenge: Extreme dimensional constraints requiring ultra-miniature camera form factors.
Solution: Ultra-compact 9mm or smaller 1080P HD miniature modules integrated with micro coax cables and flexible printed circuit boards designed for tight spatial assemblies.
Challenge: Simultaneous Localization and Mapping (SLAM) under fluctuating factory illumination.
Solution: Wide-angle (140°–180° FOV) low-distortion USB and MIPI camera modules calibrated for stereoscopic vision and real-time spatial depth mapping.
How Shenzhen’s concentrated optical component ecosystem delivers unparalleled speed-to-market, cost-efficiency, and rigorous quality control for enterprise buyers.
Shenzhen, China stands as the epicenter of global optical research, CMOS sensor packaging, and precision lens fabrication. Partnering directly with an established Shenzhen OEM/ODM camera module manufacturer offers significant competitive and strategic advantages for international buyers:
From initial optical schematic design and Gerber layout approval to physical SMT sample delivery in as fast as 10–14 working days, accelerating client design-in cycles dramatically.
Direct supply chain alliances with world-leading image sensor foundries (Sony, OmniVision, SmartSens, ON Semiconductor) ensure priority wafer allocations and favorable Bill of Materials (BOM) cost structures.
Automated SMT placement lines housed inside strict dust-free cleanrooms prevent microscopic optical contamination on sensor cover glass during lens bonding and Active Alignment procedures.
100% automated optical testing (AOI), 48-hour continuous temperature aging burn-in, vibration testing, and drop tests guarantee stable field performance prior to mass shipment dispatch.
Ensuring seamless integration into regulated international markets with comprehensive documentation and engineering support.
Deploying security camera hardware globally demands strict adherence to international safety, environmental, and cybersecurity standards. Custom camera modules manufactured by Shen Zhen You Xiang Da Technology Co., Ltd. are engineered to meet or exceed full global compliance frameworks:
Fully certified under RoHS, REACH, CE, and FCC standards. Hazardous substance restrictions strictly audited through XRF material inspection across all passive components, PCB substrates, and lens assemblies.
Flexible chip selection architectures allow system designers to specify NDAA-compliant SOC and CMOS sensor pairs, protecting client infrastructure investments in sensitive government and commercial markets.
Direct engineer-to-engineer technical support, providing custom driver configuration files (Linux V4L2 drivers, Android HAL tuning, Windows UVC inf files) to streamline host processor integration.
Detailed technical answers for hardware procurement directors, optical engineers, and embedded software architects.
Review our specialized camera modules engineered for automotive recorders, industrial vision systems, and smart home entry intercoms.
Whether you require a low-distortion USB camera module for document scanning, a high-speed MIPI vision sensor for robotics, or a wide-angle night vision module for smart security systems, our optical engineering team is ready to accelerate your project.